China Top 10 Borehole Pump Manufacturers for Global Buyers
China has become a major sourcing destination for borehole pumps, serving agriculture, construction, mining, and municipal water projects. Global buyers often find attractive pricing, broad product ranges, and flexible production capabilities. Yet a polished catalog does not always reveal how a pump performs underground.
This guide introduces ten Chinese manufacturers with relevant experience in deep-well and borehole applications. The selection considers manufacturing capability, export experience, product engineering, testing procedures, and customer support. It also examines practical details, including flow rate, total head, casing diameter, motor efficiency, stainless-steel construction, cable quality, and dry-run protection. These factors matter when a pump must operate for long hours inside a narrow, difficult-to-access well.
Performance comes first.
Reliable suppliers should provide clear curves, inspection records, warranty terms, and replacement-part support. International certifications may help, but buyers should verify their scope and validity independently. Factory audits, sample testing, and reference projects can reveal more than promotional claims. Shipping arrangements and communication quality deserve attention too, especially for remote installations.
No list is perfect. Rankings can change as factories improve, markets shift, and after-sales performance becomes clearer. Some manufacturers may excel in standard residential pumps, while others are stronger in industrial systems or customized orders. Buyers should compare each supplier against actual site conditions, not reputation alone. Before placing an order, confirm bore diameter, water chemistry, installation depth, voltage, required output, and local service expectations. A suitable pump is not merely the cheapest option; it is the one that delivers dependable water with manageable lifetime costs.
Borehole Pump Types and Their Main Applications
China Top 10 Borehole Pump Manufacturers for Global Buyers
Borehole Pump Types and Their Main Applications
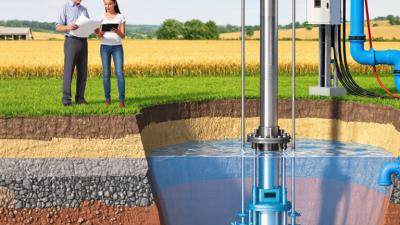
Submersible pumps sit below the water level and push water upward through rising pipes. They suit deep wells, household supply, irrigation, and livestock systems. Their sealed motors reduce priming problems, but sand can quickly damage impellers and seals. Pressure matters.
Jet pumps remain above ground and create suction through a nozzle assembly. They work best in shallow boreholes, often below 8 metres in practical installations. Maintenance is easier because technicians can reach the motor without lifting the pump. However, suction performance falls sharply with depth.
Solar submersible pumps combine photovoltaic power with a controller and storage tank. They are useful for remote farms and community water points. The International Energy Agency reported that global solar photovoltaic capacity exceeded 1,400 GW in 2023, supporting wider off-grid adoption. Yet cloudy-season storage is often underestimated.
Manual and low-lift pumps fit small communities, emergency reserves, and household gardens. They generally need less technical support than powered systems. The WHO and UNICEF Joint Monitoring Programme reported that 2.2 billion people lacked safely managed drinking water in 2022. Borehole selection therefore involves public health, not only flow rate.
Agricultural installations deserve special attention. FAO AQUASTAT estimates agriculture uses about 70% of global freshwater withdrawals. A pump with excessive capacity can waste energy and lower groundwater levels. Field inspections show that oversized systems are common. I still question simple catalogue comparisons. Actual depth, casing diameter, water quality, daily demand, and voltage should decide the specification.
China Top 10 Borehole Pump Manufacturers for Global Buyers – Borehole Pump Types and Their Main Applications
This chart compares indicative flow-rate ranges for common borehole pump types. The figures represent typical engineering applications rather than any individual manufacturer or brand.
How to read the chart: Smaller submersible pumps are commonly used for homes, livestock and remote solar systems, while larger submersible, vertical-turbine and dewatering systems are selected for irrigation, municipal water supply, mining and industrial use. Actual performance depends on borehole diameter, total dynamic head, water quality, motor power and installation conditions.
Key Criteria for Evaluating Chinese Pump Manufacturers
Evaluating Chinese borehole pump manufacturers requires more than comparing unit prices. The International Energy Agency reports that electric motor systems consume roughly 53% of global electricity. Pump efficiency therefore affects operating costs for years. Ask each supplier for tested flow, head, efficiency, power, and temperature data. A clear Q-H curve is essential. A polished catalogue is not proof.
Professional buyers should examine factory capability and product consistency. Request ISO 9001 certification, third-party test reports, material certificates, and serial-number traceability. For stainless-steel components, verify the actual grade, not only the sales description. Check motor insulation, ingress protection, cable quality, and dry-run protection. The World Bank notes that agriculture accounts for about 70% of global freshwater withdrawals, making dependable water equipment especially important in irrigation projects. Still, reliability claims can be difficult to compare. Independent verification is worth the extra time.
Tips: Send the manufacturer your real well depth, static water level, pipe length, voltage, and daily duty cycle. Ask for a sample test before a large order. Review five years of spare-parts availability and response time. A low purchase price may hide costly replacements. Also inspect packaging, because damaged cable joints and bent shafts sometimes appear after long-distance transport. Some buyers focus too heavily on efficiency and overlook local service capacity. That is a mistake worth reconsidering.
China’s Top 10 Borehole Pump Manufacturers
China’s top 10 borehole pump manufacturers serve agriculture, municipal water systems, and industrial sites worldwide. Their product ranges commonly include stainless-steel submersible pumps, deep-well motors, control panels, and replacement parts. From practical sourcing experience, buyers should compare flow rate, total head, bore diameter, cable length, and water chemistry. A low purchase price means little when a motor overheats underground. Field conditions matter.
Reliable manufacturers usually provide performance curves, motor-efficiency data, factory test records, and installation guidance. Ask for evidence, not polished promises. Check whether each pump is tested for insulation resistance, hydraulic output, vibration, and seal integrity. Export experience also matters because documentation, packaging, voltage, and service response can affect a project. Some producers offer customized impellers, frequency compatibility, and private-label production, but technical changes need written confirmation. Verifiable quality systems and traceable components strengthen buyer confidence.
The strongest candidates among China’s top 10 are not judged by brochures alone. They should explain how pumps perform in sandy water, fluctuating power, and long vertical risers. Request a sample test when the application carries serious risk. Installation feedback from distributors can reveal problems hidden in laboratory figures. A ranking is never perfect. Supplier capacity, raw-material changes, and after-sales performance can shift over time. Buyers should review recent certificates, inspect production controls, and define warranty terms before placing an order. Details matter.
Product Quality, Certifications, and Global Export Capabilities
China Top 10 Borehole Pump Manufacturers for Global Buyers
Product quality begins with controlled manufacturing, not attractive catalog photographs. Reliable manufacturers should show ISO 9001 certification, batch records, and documented inspection procedures. Buyers should request hydraulic test curves, insulation resistance results, motor efficiency data, and material certificates. These records reveal whether a pump can maintain stable pressure in deep wells.
Certifications also need careful checking. CE marking may support European sales, while other markets may require different electrical or safety approvals. Certificates should match the exact pump model, voltage, motor design, and production site. A printed certificate is not enough. Ask for recent copies and verification details.
Export capability matters when projects cross borders. Experienced suppliers provide clear packing lists, commercial invoices, spare-parts guidance, and installation manuals. They should understand voltage differences, customs documents, seaworthy packaging, and after-sales communication. A well-packed pump arrives with protected cable ends and dry, labeled components. Small details matter.
Field performance can still vary. Water quality, sand content, cable length, and unstable power may reduce service life. Some suppliers explain these risks clearly; others focus only on maximum flow. That is a warning sign. A practical comparison should include warranty terms, response time, replacement procedures, and local technical support. Even careful buyers can overlook pump cooling requirements. Mistakes happen. The best manufacturers respond with evidence, not promises.
How Global Buyers Can Select the Right Manufacturer
China Top 10 Borehole Pump Manufacturers for Global Buyers
A top-ten list can narrow your search, but it cannot replace technical verification. The right manufacturer should match your borehole diameter, required flow, total head, and water chemistry. Ask for pump curves tested under defined conditions, not only attractive catalog figures. Confirm motor efficiency, cable quality, insulation class, sealing design, and protection against dry running. Stainless steel components may be essential where water contains sand or corrosive minerals.
Supplier reliability matters as much as pump performance. Request factory test records, material certificates, quality-control procedures, and traceable serial numbers. Check whether the manufacturer can provide compatible spare parts after installation. Clear warranty terms should define response times, exclusions, and responsibility for transport. Independent certifications can support confidence, but they should be verified against the exact model. A certificate for one pump does not automatically cover every product.
Tips: Send the same specification sheet to each candidate. Compare like for like. Ask for references from projects with similar depth and operating conditions. If possible, arrange a video factory audit or an on-site inspection. Review packaging details, because damaged cable ends or poorly protected couplings can create costly delays. Do not choose by price alone. I have seen buyers overlook after-sales support, then discover that a small seal was unavailable locally. No checklist is perfect. Leave room for technical discussion, because the first specification may be incomplete.